BORING BAR ISO P - LEFT HAND_PCLN(RL) INT
Caution
Product Description
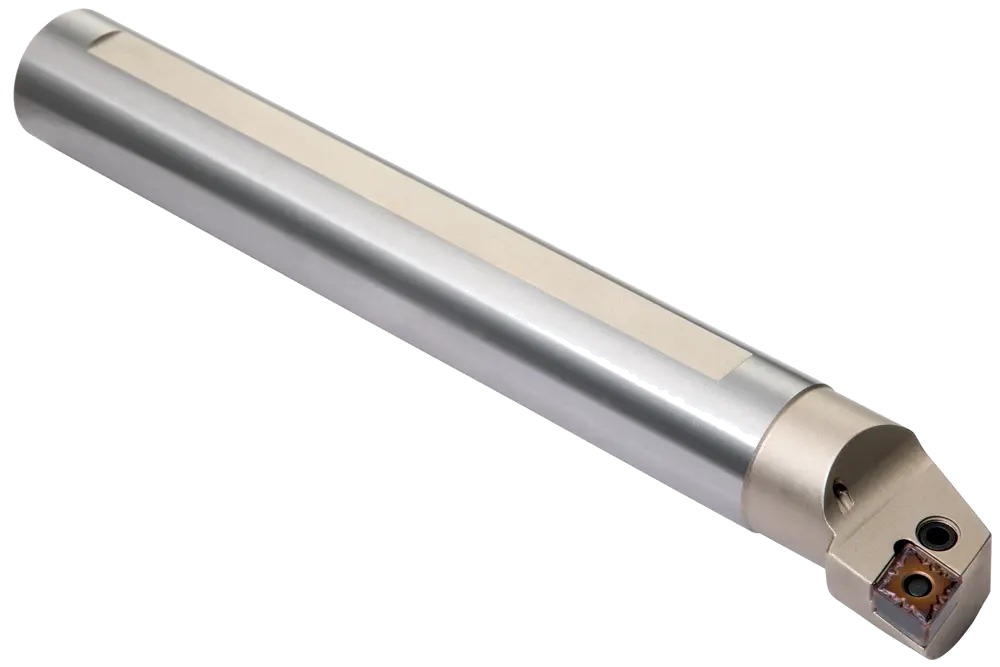
DORMER PRAMET A16M-PCLNL 09 is a left-hand, lever lock (ISO P clamping) steel boring bar with a 16 mm shank, 150 mm overall length and an internal coolant hole. It holds 80° rhombic negative CN.. 0903.. inserts at a 95° lead angle for internal longitudinal turning, shoulder machining and taper boring in bores from 20 mm in diameter.
General information
- Manufacturer: DORMER PRAMET (Pramet brand). Material ID 6761029, EAN 3603602963758.
- Series: PCLN internal boring bars. The mirror-image right-hand version is A16M-PCLNR 09 (Material ID 6761030).
- Inserts are sold separately. Use negative CN.. 0903.. inserts (for example CNMG 0903..).
Reading the ISO code A16M-PCLNL 09
- A: steel bar with internal coolant supply
- 16: shank diameter 16 mm
- M: overall length 150 mm
- P: lever lock clamping through the insert hole
- C: 80° rhombic insert shape
- L: 95° tool style (side and end cutting)
- N: 0° insert clearance angle (negative insert)
- L: left-hand version
- 09: insert size
Usage guidance
- Check the minimum bore diameter (Dmin 20 mm) before machining. The boring bar cannot enter smaller holes.
- Set the cutting corner at spindle centre height, and use the flat on the shank to orient the boring bar in the holder or sleeve.
- Keep the overhang as short as possible. For steel boring bars, an overhang of up to about 3 × D is a common guideline; longer overhangs increase the risk of vibration.
- Connect the coolant supply to the coolant hole to improve chip evacuation, especially in deep or blind bores.
- Before cutting, check that the left-hand boring bar matches the spindle rotation direction and tool position on your machine.
- Clean the insert pocket before indexing or replacing the insert, and tighten the clamping screw securely.
Overview
The A16M-PCLNL 09 (Material ID 6761029) belongs to the DORMER PRAMET PCLN internal boring bar range. It is a lever lock boring bar that clamps an 80° rhombic negative insert with a 9.525 mm inscribed circle and 3.18 mm thickness (ISO designation CN.. 0903..). The tool is left-hand, cuts on both side and end at a 95° lead angle, and has an off-set steel shank of 16 mm diameter and 150 mm length with a through-coolant hole.
Key features
- P-type lever lock (hole clamping): the insert is held through its central hole, leaving the top face free for unobstructed chip flow.
- Uses double-sided negative CN.. 0903.. inserts, giving up to 4 usable cutting corners per insert for a low cost per edge.
- The 95° lead angle allows longitudinal boring, facing up to a shoulder and taper boring with one tool.
- The internal coolant hole directs coolant to the cutting zone, helping chip evacuation from the bore and extending tool life.
- Designed for finishing, medium machining and roughing, and suitable for stable, unstable and heavy working conditions.
Typical applications
- Internal longitudinal turning with shoulder (primary use)
- Internal longitudinal turning without shoulder (primary use)
- Internal cone (taper) turning (primary use)
- Chamfering (bevelling) in the hole (possible use)
| Item | Specification |
|---|---|
| Brand | DORMER PRAMET |
| Tool type | Boring bar, ISO P lever lock (hole clamping) |
| Holder style | PCLN, internal |
| Hand | Left hand (L) |
| Body material | Steel, off-set shank |
| Coolant | Through-tool (internal coolant hole) |
| Compatible insert | CN.. 0903.. (80° rhombic, negative) |
| Insert IC / thickness | 9.525 mm / 3.18 mm |
| Lead angle | 95° |
| Shank diameter | 16 mm |
| Overall length | 150 mm |
| Minimum bore diameter | 20 mm |
| Ordering code | Material ID | Hand | Insert | D (mm) | l1 (mm) | f (mm) | h (mm) | Dmin (mm) | Lead angle | Orthogonal rake | Coolant |
|---|---|---|---|---|---|---|---|---|---|---|---|
| A16M-PCLNL 09 | 6761029 | Left | CN.. 0903.. | 16 | 150 | 11 | 15 | 20 | 95° | -5° | Internal |
Cylindrical steel boring bar with an off-set cutting head at the front end and a ground flat along the shank.
- D: shank diameter 16 mm
- l1: overall length 150 mm
- h: shank height across the flat 15 mm
- f: distance from the bar axis to the cutting corner 11 mm
- Dmin: minimum bore diameter 20 mm
- Insert pocket for an 80° rhombic CN.. 0903.. insert, set for left-hand cutting at a 95° lead angle
- Coolant hole running through the shank to the cutting head
Choosing an insert for the workpiece material
- Steel (ISO P): a general-purpose CN.. 0903.. insert with a steel grade and a medium chipbreaker.
- Stainless steel (ISO M): a sharp edge and a tough grade to limit built-up edge and work hardening.
- Cast iron (ISO K): a strong edge with a wear-resistant grade.
- Heat-resistant alloys and titanium (ISO S): a sharp, positive chipbreaker to keep cutting forces low.
Choosing the nose radius
In boring, a smaller nose radius such as 0.4 mm (CNMG 090304) reduces radial cutting force and vibration. A larger radius such as 0.8 mm (CNMG 090308) gives a stronger edge for roughing.
Choosing the bar size
Use the largest bar diameter that fits the bore. For bores of 25 mm and above, the A20Q-PCLNL 09 (20 mm shank, 180 mm length, Dmin 25 mm) is more rigid and uses the same insert.
About the name ISO P
ISO P in the series name refers to the P clamping system (lever lock through the insert hole), not to the ISO P workpiece material group. The boring bar can machine steel, stainless steel, cast iron and other materials, depending on the insert grade fitted.