Linear Shafts Both End Threaded with Wrench Flats

Brand :
MISUMI
Caution
- Some Page Materials are under updating.
- Download Free! >> Economy Series Catalog (TH-EN-FY25) CLICK here
Product Description
[Features]
• High-precision linear guide shaft for use with linear bearings and bushing-type products.
• Material options include 45 or GCr15 and SUS440C or equivalent high-hardness corrosion-resistant steel.
• Hard chrome plating options support rust-prevention selection where required.
[Use]
• Please check the specifications before purchasing to ensure the product is suitable for the intended application.
Product Overview
The linear guide shaft is a high-precision shaft product that can be used in combination with linear bearings and other bushing-type products. It not only offers excellent wear resistance, but also provides a variety of additional processing options.
Dimensional Drawing
Note: When B=0 or S=0, it indicates no threads.


Material Specifications
| Type |  Material |  Hardness |  Surface Treatment | D (mm) | L (mm) | |
| With Wrench Slot Type | ||||||
| Standard Type | ||||||
| D Tolerance g7 | D Tolerance f8 | |||||
| E-SFAU | - | 45 or GCr15 | High-frequency quenching For effective hardened layer depth, please click  Surface Hardness Reference 45 or GCr15 55HRC~ SUS440C or equivalent high-hardness corrosion-resistant steel 53HRC or more | - | 6 to 50 | 25 to 1496 |
| E-SSFAU | - | SUS440C or equivalent high-hardness corrosion-resistant steel | ||||
| E-PSFAU | - | 45 or GCr15 | Hard chrome plating Plating hardness HV750~ Plating thickness 3µ or more | |||
| E-PSSFAU | - | SUS440C or equivalent high-hardness corrosion-resistant steel | ||||
| - | E-PSFGU | 45 | - | Hard chrome plating Plating hardness: HV750~ Plating thickness: 10µ or more | ||
 The machined part at the shaft end (effective thread length + approx. 10 mm) may have reduced hardness due to the annealing effect of machining.If rust prevention is required, please give priority to products with hard chrome plating Surface Treatment. Please click Rust Prevention MethodsIf used together with linear bearings, please choose products with high-frequency quenching.
Alterations
| Alterations | Code | Spec. | |||
 | LKC | Change L dimension tolerance Ordering Code LKC When using LKC, the unit specified for the L dimension can be 0.1 mm L<200 → L±0.03200 ≤ L<500 → L±0.05 L ≥ 500 → L±0.1 | |||
 | FC | ||||
 | WFC | ||||
 | SX | ||||
 | PC QC | PC: Perform undercut machining on the P dimension section. QC: Perform undercut machining on the Q dimension section. Ordering Code PC For details on undercut machining dimensions, please refer to P.37Applicable conditions Applicable for M ≥ 6  Not applicable for D = Q or D = P | |||
 | RC | Add one flat surface at a 90-degree position Ordering Code RC10 Applicable conditions Applicable for D=10 to 30 Cannot be used together with WRC | |||
 | WRC | Add flat machining at two 90-degree positions Ordering Code WRC10-Y10 Applicable conditions Applicable for D=10 to 30 Cannot be used together with RCCannot be machined on the same plane | |||
 | PMC PMS QMC QMS | Change the external thread to a fine thread PMC·QMC: Fine thread pitch suitable for bearing locknuts PMS·QMS: Fine thread pitch suitable for cylinders | |||
When selecting multiple additional machining operations, there must be a gap of at least 2 mm between the machined areas.Additional machining may result in reduced hardness. Please refer to P.36Specification Table
| Part Number | Specified unit: 1 mm | P·Q Selection | Wrench Slot Size | (Y) Max. | |||||||||||||||
| Type | D | L | F·T | B·S | SC | W | ℓ1 | ||||||||||||
| Standard Type (With Wrench Slot) (D Tolerance g7) E-SFAU E-SSFAU E-PSFAU E-PSSFAU (D Tolerance f8) E-PSFGU | 6 | 25–896 | 2 ≤ F ≤ P × 5 2 ≤ T ≤ Q × 5 | (When P ≤ 6) B ≤ F-2 (When P = 8 or 10) B ≤ F-3 (When P ≥ 12) B ≤ F-5 (When Q ≤ 6) S ≤ T-2 S ≤ T-3 (When Q ≥ 12) S ≤ T-5 (When there is no thread) B = 0 S = 0 B·S ≥ pitch×3 | 3 | 4 | 5 | SC = specified unit 1 mmSC + ℓ1 ≤ LSC ≥ 0Wrench slot details >>See (PDF) | 5 | 8 | 900 | ||||||||
| 8 | 25–1096 | 3 | 4 | 5 | 6 | 7 | 1100 | ||||||||||||
| 10 | 25–1196 | 3 | 4 | 5 | 6 | 8 | 8 | 1200 | |||||||||||
| 12 | 25–1396 | 3 | 4 | 5 | 6 | 8 | 10 | 10 | 10 | 1400 | |||||||||
| 13 | 25–1396 | 4 | 5 | 6 | 8 | 10 | 12 | 11 | 1400 | ||||||||||
| 15 | 25–1396 | 4 | 5 | 6 | 8 | 10 | 12 | 13 | 1400 | ||||||||||
| 16 | 25–1396 | 4 | 5 | 6 | 8 | 10 | 12 | 14 | 1400 | ||||||||||
| 20 | 25–1396 | 5 | 6 | 8 | 10 | 12 | 16 | 17 | 1400 | ||||||||||
| 25 | 25–1396 | 6 | 8 | 10 | 12 | 16 | 20 | 24 | 22 | 1400 | |||||||||
| 30 | 25–1496 | 8 | 10 | 12 | 16 | 20 | 24 | 27 | 15 | 1500 | |||||||||
| 35 | 25–1496 | 10 | 12 | 16 | 20 | 24 | 30 | 30 | 1500 | ||||||||||
| 40 | 25–1496 | 12 | 16 | 20 | 24 | 30 | 36 | 20 | 1500 | ||||||||||
| 50 | 25–1496 | 16 | 20 | 24 | 30 | 41 | 1500 | ||||||||||||
Outer diameters 35, 40, and 50 are only available for E-PSFAU specifications.| D Tolerance | ||
| D | g7 | f8 |
| 6 | -0.004 -0.016 | -0.010 -0.028 |
| 8 | -0.005 -0.020 | -0.013 -0.035 |
| 10 | ||
| 12 | -0.006 -0.024 | -0.016 -0.043 |
| 13 | ||
| 15 | ||
| 16 | ||
| 18 | ||
| 20 | -0.007 -0.028 | -0.020 -0.053 |
| 25 | ||
| 30 | ||
| 35 | -0.009 -0.034 | - |
| 40 | ||
| 50 | ||
Product Features
Feature 1: Offers high-precision dimensional tolerances and is widely used in various precision equipment.
Feature 2: Uses bearing steel with excellent wear resistance (45 or GCr15) and SUS440C or equivalent high-hardness, corrosion-resistant steel, which undergo high-frequency quenching to enhance wear resistance while maintaining original toughness.
Feature 3: Various additional processing options are available to meet different usage environments.
Feature 4: Typically used in combination with linear bearing products, it provides excellent linear guidance. Compared to standard shaft and bushing structures, even during high-speed reciprocating motion, there is minimal wear.
Feature 5: Hard chrome plating is available as a Surface Treatment, offering excellent rust resistance. The coating hardness reaches HV750, so it will not be easily worn even when used with high-hardness workpieces.
Feature 2: Uses bearing steel with excellent wear resistance (45 or GCr15) and SUS440C or equivalent high-hardness, corrosion-resistant steel, which undergo high-frequency quenching to enhance wear resistance while maintaining original toughness.
Feature 3: Various additional processing options are available to meet different usage environments.
Feature 4: Typically used in combination with linear bearing products, it provides excellent linear guidance. Compared to standard shaft and bushing structures, even during high-speed reciprocating motion, there is minimal wear.
Feature 5: Hard chrome plating is available as a Surface Treatment, offering excellent rust resistance. The coating hardness reaches HV750, so it will not be easily worn even when used with high-hardness workpieces.
Precautions
 | (2) Reduced hardness in machined areas After quenching the base material, machining may cause reduced hardness due to annealing in the following areas: - All external threads - All steps - Internal threads: When M ≥ D/2, double-hole internal threads, and hard chrome plated products made of SUS440C or other high-hardness corrosion-resistant steels - Additional machining of wrench slots (SC-WSC-SX) - Additional machining of flat surfaces (FC-WFC) - Additional machining of V-grooves (VC-WVC) - Except for fully hardened types. |
Only the shaded area in section D is hard chrome plated.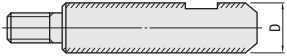 | (3) Plating after Surface Treatment After Surface Treatment of the base material, machining is performed, and the following areas are not plated: - Groove areas -External thread sections -Internal thread sections -Wrench slots, V-grooves, flat surfaces, and cut surfaces -The inside of pipe-type guide shafts is not hard chrome plated and may rust. |
Example of Use


Application Industries
| Medical | Semiconductors | Electronics and Electrical Appliances | ||
 |  |  | ||
| Smartphones | Food | Automotive | ||
 |  |  |
Related Products
| Linear Bearing Standard Type, Straight Cylinder Type | Bearing Housing Assembly T Type | Retaining Ring Open Type | ||
 |  |  | ||
| Representative model: LMU6 | Representative model: BGHFS6000ZZ-30 | Representative model: PSCS10-10 | ||
| Advantages: High quality, low price, short lead time | Advantages: Complete range, high precision and high quality | Advantages: Supporting shaft products, complete range |
Related Documents
Corrosion resistance of metal materials and Surface Treatments Click  Corrosion Resistance Table